
A sandblasting operation running a 15 kW machine just 10% short of its rated air delivery can waste $900 a year at 6,000 hours and $0.10/kWh. The problem is rarely the blast media or the operator. It is a sandblasting screw air compressor sized for peak pressure instead of continuous flow.
Sandblasting is close to a 100% duty-cycle application. The nozzle pulls air the whole time it is open, and any shortfall shows up immediately as slower cleaning, more abrasive use, and overtime. Sizing starts with the nozzle demand, not with the largest motor on the quote.
The 5 sizing checks before you buy
- Continuous free air delivery. Confirm the rated m³/min or cfm is at the blast pressure you will actually run, not at a lower pressure.
- Pressure at the nozzle. A pressure drop of 0.5 bar through hoses, filters, and fittings forces the compressor to work harder or the blast to slow down.
- Moisture removal. A refrigerated dryer and filter protect dry abrasive from clumping and prevent wet air from damaging the blast pot.
- Dust protection. Blast rooms are dusty. The compressor needs a protected intake and filtration that can survive abrasive fines.
- Duty cycle and load profile. One full-time blast nozzle needs continuous capacity; multiple intermittent users may justify a different control strategy.
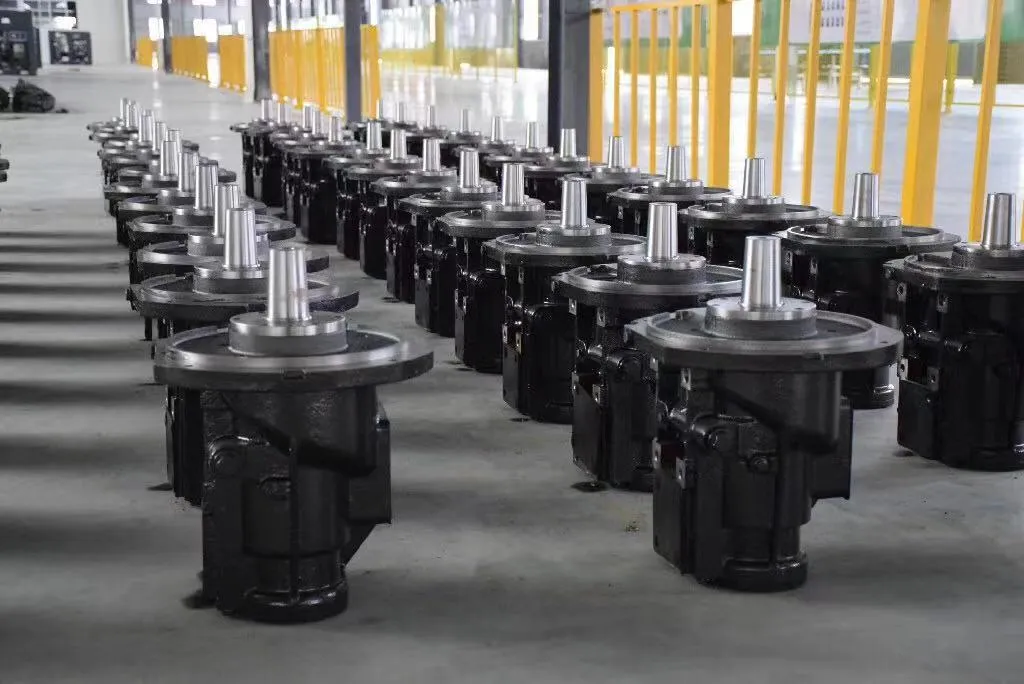
Panrui’s screw air compressor range covers 7.5–315+ kW, 3–13 bar, and 1.1–53.0 m³/min. That range is useful only when you compare the nozzle’s actual demand against a machine that can hold the required FAD at your working pressure.
Why continuous FAD matters more than tank size
An air receiver can smooth pressure pulses, but it cannot create air. If the blast nozzle needs 10 m³/min at 7 bar and the rotary screw air compressor only delivers 8 m³/min at that pressure, the tank will drain and the nozzle will starve no matter how large the receiver is.
Add a 20% margin for line losses, filter loading, and future blast equipment. Then request the compressor’s FAD and specific power at exactly that corrected volume and pressure. The lower the specific power in kW per m³/min, the less electricity you pay for the same blasting output.
Apply the same rule to any energy-saving promise. Panrui positions its screw air compressor package as cutting operational costs by up to 30%, but the claim is only useful when the before and after comparison uses the same FAD, pressure, and annual blasting hours.
When a VSD helps, and when it does not
A variable speed screw air compressor pays off when blasting demand rises and falls across shifts. For one nozzle running flat-out all day, a correctly sized fixed-speed machine can be simpler and cheaper to maintain. Match the control type to the load profile instead of paying for turndown you will never use.
What buyers get wrong
- Buying horsepower instead of flow. Motor kW is an input. FAD at working pressure is the air the nozzle receives.
- Ignoring pressure drop. Undersized piping and dirty filters can erase the compressor’s rated output.
- Skipping the dryer. Wet compressed air turns dry blast media into a clogging, inconsistent mess.
- Choosing the lowest first cost. A machine that runs short forces longer blast cycles and higher energy and labor cost.
Turn the sizing into a purchase decision
Fix three numbers before you compare quotes: required FAD at the nozzle, working pressure, and annual blasting hours. Then ask for the sandblasting screw air compressor data at that exact operating point, including package input power and specific power. Compare annual energy cost, not just the purchase price.
Need a like-for-like calculation for your blast room? Contact Panrui with your nozzle flow, pressure, and running hours for a specific model recommendation.