
One pressure dip on a two-piece can line does more than dent a few cans. A bodymaker that loses air mid-stroke jams, and a necker that sees 5.5 bar instead of 6.0 bar misfires on every cycle. On a 2,000-cans-per-minute line, twenty minutes of lost production is 40,000 cans of scrap. These failures usually trace back to one choice: the screw air compressor for can manufacturing was selected on price, not on the six specs the process needs.
Why Can Lines Are Harder on Air Than Most Plants
Can manufacturing packs enormous air demand into short, violent bursts. Blow-off jets strip lubricant from cup walls at high speed, air conveyors float cans through the necker and flanger, and inspection jets reject defects in milliseconds. Unlike a stamping press that draws air smoothly, a can line pulses, and every pulse must hold pressure within a tight band.
- Bodymaker and trimmer blow-off demand spikes to 100% of rated flow in under a second.
- Airveyors stall and double-feed when pressure sags mid-transfer.
- Necking and flanging misform cans when supply air oscillates, turning good metal into scrap.
The result is a hard stop: a jammed bodymaker, a rethread, and a line that sits idle while labor cost and delivery deadlines keep running. The right rotary screw air compressor removes that failure mode instead of patching it.
6 Specs That Keep a 24/7 Can Line Running
1. Constant-pressure variable-speed control
A variable-speed drive holds discharge pressure inside a narrow band as demand spikes and falls. That matters twice over: the line never sees a sag deep enough to misfire, and you stop paying for pressure you do not need. Every extra 1 bar of set pressure costs roughly 8% more power, so a unit tuned to the true 6.0 bar need pays back fast.
2. Two-stage compression with low specific power
Specific power, measured in kW per m³/min, is the number that predicts your electricity bill. A two-stage screw compressor compresses in two steps, lowering the power consumed per unit of air. In comparable 90 kW machines, a single-stage unit runs around 7.0 kW/(m³/min) while a two-stage air-cooled unit reaches about 5.9 kW/(m³/min), roughly 15% less electricity for the same air.
3. Oil-free Class 0 air for product-contact surfaces
Any jet that touches the inside of a food or beverage can must not carry oil. Specify an oil-free screw air compressor that meets ISO 8573-1 Class 0 for blow-off and inspection air. Oil-injected units are fine for general plant air, but a filter chain cannot make them acceptable on direct product-contact surfaces.
4. Cooling built for a 52°C plant, not a 40°C office
Can lines run through the hottest months without stopping, and compressor rooms rarely stay cool. A unit designed for 52°C ambient with an oversized cooling system keeps running when a standard 40°C-rated machine trips on high temperature and takes the line down with it.
5. Dry air for airveyors and vision inspection
Moisture condensing in airveyor channels and inspection optics causes double feeds and false rejects. Pair the compressor with a matched dryer and keep dew point low enough that no water forms at line pressure. Dry, stable air keeps a high-speed line reading cans correctly instead of rejecting good product.
6. Remote monitoring and a proven run-in
Buy a machine that was factory-tested under continuous load before shipping and that reports pressure, temperature, and runtime remotely. A 12-hour uninterrupted factory run-in catches assembly faults before they become your midnight line stop, and remote monitoring lets you see a cooling or pressure trend before it trips the line.
The Energy Math Behind These Specs
The savings stack. Pressure tuning alone is worth about 8% per bar you remove. The two-stage architecture adds roughly another 8%, and a full efficiency package—low-resistance intake filtration, oversized aftercooler, oil-cooled motor, and optimized recycle control—can total about 21% lower energy than a standard single-stage machine.
Put that against a 90 kW machine running 24/7. A 15% reduction in specific power, from 7.0 to 5.9 kW/(m³/min), cuts roughly 13 kW of demand for the same output. Over 8,000 running hours a year, that is on the order of 100,000 kWh a year that never shows up on the bill.
What Buyers Usually Get Wrong
“A bigger receiver tank will cover the dips.” A tank buffers seconds, not minutes. A sustained sag during a blow-off burst needs reserve flow and fast control, not more stored volume.
“Oil-injected air is fine for cans.” It is not fine on surfaces that touch food or beverage. Keep oil-injected air on general plant duty and use Class 0 oil-free air anywhere product is contacted.
“Just buy an 8 bar machine for headroom.” That headroom costs about 8% of your power per extra bar, every hour the line runs. Size to the true demand and let the drive hold it steady.
Next Step
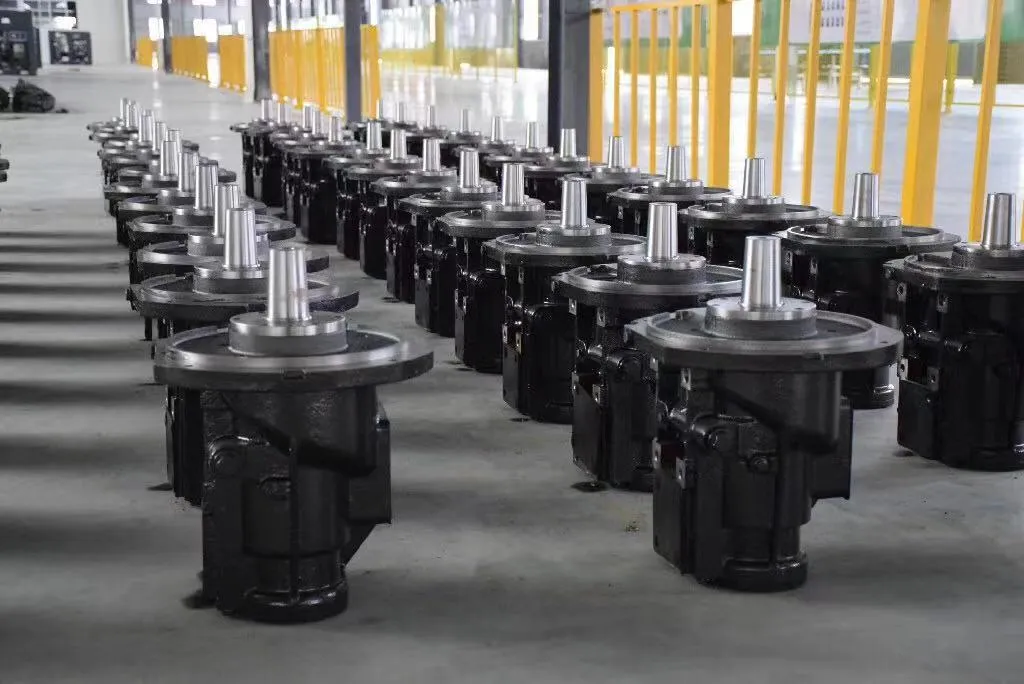
Send your line speed, can size, and peak m³/min to a supplier that sizes from the process backward. Start from the full rotary screw air compressor range, confirm the specific-power number on the data sheet, and get the Class 0 and cooling ratings in writing before you pay. A can line that never stops is worth more than the discount on the wrong machine.