
A tube mill does not forgive a 0.5 bar drop at the weld squeeze roll. When compressed air pressure sags mid-coil, the squeeze cylinders lose grip, the weld wanders, and the mill either rejects the coil or ships seam defects that come back as claims. The fix is not “a bigger compressor” — it is a screw air compressor for tube mills specced for steady pressure, mill-scale dust, and 24/7 duty, with the lowest specific power you can prove.
Below are the six specs that matter, plus the energy numbers you should ask every supplier to put in writing before you sign.
Why Tube Mills Starve Their Compressed Air System
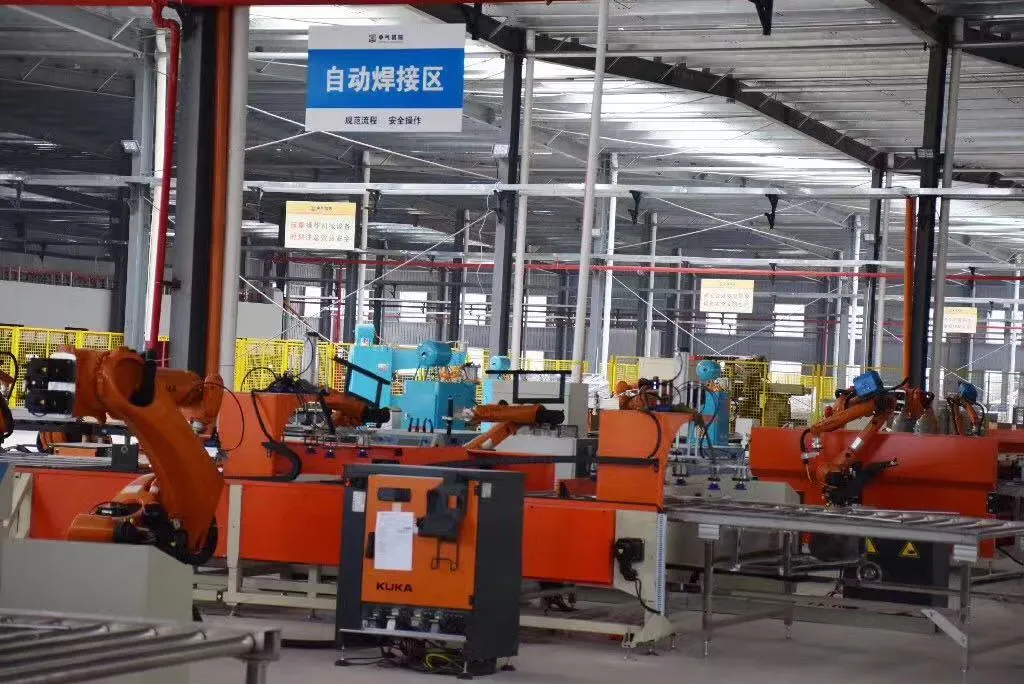
ERW and HFW tube mills run coiled steel through forming stands, a weld squeeze, a scarfing station, and a flying cut-off — usually around the clock. The pneumatic loads are short and violent: clamp cylinders fire, edge guides correct, the cut-off saw cycles, and hydrostatic testers seal and pressurize test pieces. Every one of those pulses drops line pressure.
Two site conditions make it worse. First, mill scale and coolant mist load the intake air with fine, abrasive dust that plugs filters fast. Second, the compressor room is often next to the mill floor, where ambient temperature swings with each coil change. A machine sized on motor kW alone — with no reserve for pressure recovery — will lag behind every pulse, and the weld is the first thing to suffer.
The 6 Specs That Keep Weld Pressure Stable
- Specific power, not motor kW. Compare kW per m³/min, not nameplate power. A 37 kW single-stage unit at 7.2 kW/(m³/min) delivers less air per unit of electricity than a two-stage unit at 6.5 kW/(m³/min) — a 9.7% gap that compounds every hour the mill runs.
- Pressure reserve at the squeeze. Specify rated pressure at least 1 bar above the weld station’s requirement, and check pressure recovery time after a cut-off cycle.
- Two-stage compression for continuous duty. Splitting compression into two stages cuts the work lost to heat and lifts volumetric efficiency. On Panrui’s measured data the two-stage airend alone accounts for roughly 8% of a 21.2% total saving.
- Dust-rated intake filtration. Mill scale is conductive and abrasive. A filter that drops intake resistance from 1600 Pa to 800 Pa protects the airend and defends the specific-power number.
- Oil-cooled motor and a bigger aftercooler. These hold discharge temperature down so the dryer works less and the oil stays in spec during 24/7 summer runs.
- Pressure customization to actual demand. Every 1 bar of unnecessary pressure costs about 8% in energy. Matching the setpoint to the mill’s true requirement is the fastest zero-capital saving.
The Number That Separates a Quote From a Power Bill
Specific power is the honest metric: electricity in, air out. When you compare machines, look past the cabinet and check the rotary screw air compressor specific-power curve at your real operating pressure. Panrui’s comparison sheet shows a 75 kW single-stage screw at 6.9 kW/(m³/min), while a two-stage vertical unit of the same power sits at 6.0 kW/(m³/min). Over a 24/7 mill schedule that difference is not a rounding error — it is a permanent reduction in every kWh the plant buys.
The savings stack. An optimized intake (0.2%), full-synthetic oil (1%), pressure customization (8%), a larger aftercooler (1%), cooler intake air (0.5%), an oil-cooled motor (0.5%), recirculation-valve control (2.5%), and the two-stage airend (8%) add up to roughly 21% — before you even touch the leaks in the pipe run.
For the buyer, this means the quote that looks cheap on motor kW is usually the expensive machine on the meter. A two-stage screw air compressor quoted against a single-stage unit should be judged by specific power and total cost of ownership, not sticker price.
One Bar You Do Not Need Costs 8%
Most mills run the header hotter than the process needs “just to be safe.” That safety margin has a price: each extra bar costs about 8% in specific power. Before adding another compressor, map the real pressure at the weld, the testers, and the air tools. In most plants a one-bar correction is worth more than a new machine.
A variable speed screw air compressor earns its keep on a tube mill because demand pulses with coil changes. VSD holds the setpoint through the pulses instead of running unloaded between them.
What Buyers Get Wrong
- Buying on motor kW. Two machines with the same kW can differ by 10% or more in air delivered. Ask for the specific-power curve at your pressure.
- Ignoring dew point. Moisture in weld-station air pits valves and clouds the hydro tester. Size the dryer with the compressor, not after it.
- No dust plan. A compressor fed unfiltered mill air wears its airend early. Demand the intake pressure-drop figure in writing.
Get a Spec, Not a Sales Pitch
If your tube mill is tripping on low pressure, overheating in summer, or burning through filters, start with the six specs above and a specific-power comparison at your real operating pressure. Send us your demand profile — coil widths, line speed, weld pressure, and duty hours — and we will return a matched recommendation with the numbers attached. Contact us for a spec sheet and an energy calculation for your line.